

10 Common Design Flaws in Production Lines that Reduce MTBF
- Kerin Epperly, CLSSMBB
- Jul 29
- 36 min read
When a production line is poorly designed, the equipment starts showing clear signs of distress. Bearings fail prematurely, couplings loosen, conveyors jam, and operators develop workarounds that bypass intended processes. Maintenance teams spend more time fixing breakdowns than preventing them. Many companies blame maintenance practices, but often the real problem lies in the layout of the production line itself. This blog explores the top 10 failure fingerprints that reveal how your production line design may be destroying your Mean Time Between Failures (MTBF).
Reliability Crime Lab Recommendation:
Focus on one design flaw each month during operator training. Avoid overwhelming operators with too many concepts at once. Instead, dedicate each month to a single design flaw, teaching employees how to recognize its failure fingerprints, understand why it occurs, and identify where it exists on their own production line. Consistent monthly practice builds pattern recognition skills that help operators detect problems earlier, communicate more effectively with maintenance, and prevent failures before they become downtime.
1. Poor Foundation Design and Settlement
Description and Impact
Every production line begins with its foundation. A properly designed foundation supports equipment loads, absorbs operating forces, minimizes vibration, and maintains precise machine alignment throughout the equipment's life. When foundations are improperly designed, inadequately supported, or settle unevenly over time, machines gradually shift from their original positions. This movement introduces additional stress into rotating equipment, accelerates component deterioration, and creates chronic reliability problems throughout the production line.
Layout Problem
The production line was installed on a foundation that cannot adequately support the equipment or maintain long-term alignment.
Poor soil preparation,
insufficient concrete thickness,
inadequate reinforcement,
deteriorated grout, or improper anchoring
Allows equipment to shift during normal operation. Because production equipment is interconnected, movement of one machine often transfers additional stress to adjacent equipment, allowing deterioration to spread throughout the production line.

Failure Fingerprints
Bearings repeatedly fail at the same machine.
Couplings require frequent realignment.
Mechanical seals leak prematurely.
Elevated vibration levels are detected.
Anchor bolts repeatedly loosen.
Grout or concrete cracks around equipment bases.
Shafts show signs of chronic misalignment.
Thermal imaging identifies overheated bearings or couplings.
Precision alignment does not remain within tolerance.
Nearby connected equipment begins experiencing similar failures.
Fingerprints Point Toward the Type of Issue
These fingerprints suggest investigators should examine:
Uneven foundation settlement.
Inadequate soil preparation.
Cracked or deteriorated concrete.
Damaged or missing grout beneath equipment.
Loose or improperly installed anchor bolts.
Inadequate structural support.
Excessive vibration transmitted through the foundation.
Equipment installed on unstable or unsupported flooring.
Fix-and-Go Issue
Maintenance repeatedly replaces bearings, couplings, seals, and other worn components while performing precision shaft alignments. The equipment returns to service, but the same failures continue because the supporting foundation continues to move. Until the structural problem is corrected, the production line will continue to experience recurring failures regardless of how many components are replaced.
Correct the Design So It Doesn't Happen Again
Once foundation movement or settlement has been identified as the root cause, the objective is to stabilize the equipment rather than continually replacing the components damaged by misalignment and vibration. The following engineering improvements address the source of the problem:
Conduct a structural assessment to determine the extent of foundation settlement or deterioration.
Repair or replace cracked or deteriorated concrete foundations.
Regrout equipment bases using the appropriate non-shrink grout.
Tighten or replace damaged anchor bolts and verify proper torque specifications.
Relevel equipment and perform precision shaft alignment after foundation repairs are completed.
Reinforce or enlarge the foundation if it is undersized for the equipment's operating loads.
Improve soil stabilization or support where settlement continues to occur.
Install vibration isolation where appropriate to reduce the transmission of dynamic forces.
Verify that the foundation is capable of supporting both the static weight and dynamic operating forces of the equipment.
Inspect adjacent equipment to ensure foundation movement has not affected machine alignment throughout the production line.
Establish routine inspections of grout, anchor bolts, concrete, and foundation condition to detect deterioration before it affects equipment reliability.
Confirm equipment alignment after major repairs, relocation, or seismic events.
The goal is to eliminate the structural conditions that caused the misalignment. Once the foundation is stable, equipment maintains its alignment, vibration decreases, component life increases, and the production line operates with significantly greater reliability.
Prevention and Best Practices
The foundation is the structural backbone of the production line. A properly designed and installed foundation provides the stability necessary for equipment to operate within its design tolerances throughout its entire service life. Investing in foundation design during construction prevents years of chronic reliability problems.
Perform a geotechnical investigation before construction to evaluate soil conditions, load-bearing capacity, drainage characteristics, and settlement potential.
Design foundations to support both the static weight of the equipment and the dynamic forces generated during operation.
Size foundation pads and reinforcement according to equipment loads and manufacturer recommendations.
Install anchor bolts, base plates, and grout using approved installation procedures and verify proper alignment before equipment startup.
Ensure concrete foundations are properly cured before installing and commissioning production equipment.
Incorporate vibration isolation or damping systems where equipment generates significant dynamic loads.
Design adequate drainage around foundations to prevent erosion, soil saturation, frost heaving, and long-term settlement.
Verify foundation elevations, flatness, and levelness during construction and before equipment installation.
Conduct precision alignment of rotating equipment after installation and again after initial operating conditions stabilize.
Periodically inspect foundations, grout, anchor bolts, and support structures for cracks, movement, corrosion, or signs of settlement.
Recheck equipment alignment after significant maintenance activities, heavy impacts, seismic events, or facility modifications.
Document foundation inspections, alignment measurements, and settlement observations as part of the facility's long-term reliability program.
A production line can never be more reliable than the foundation supporting it. When foundations are properly engineered, installed, and maintained, equipment remains aligned, vibration is minimized, structural fatigue is reduced, and the entire production system operates more reliably with fewer unexpected failures and a significantly higher Mean Time Between Failures (MTBF).
Reliability Impact
Foundation problems increase vibration, accelerate bearing wear, loosen fasteners, shorten coupling life, damage mechanical seals, and create chronic shaft misalignment. The result is increased maintenance costs, more unplanned downtime, reduced Mean Time Between Failures (MTBF), and lower overall equipment reliability. A reliable production line begins with a stable foundation because every machine depends on it.
2. Poor Machine Transitions
Description and Impact
The transition between two pieces of equipment is often where production problems begin. When conveyors, guide rails, starwheels, timing screws, or transfer plates are poorly aligned or improperly designed, products become unstable as they move from one machine to the next. Instead of flowing smoothly, products tip, bounce, rotate, or jam. These repeated impacts place unnecessary stress on both the product and the equipment, accelerating wear and reducing overall production reliability.
Layout Problem
The production line was designed with poor machine-to-machine transitions. Equipment elevations, conveyor spacing, transfer plates, and guide systems do not provide continuous, controlled product movement. Products lose stability as they move between machines, creating repeated impacts and mechanical interference.

Failure Fingerprints
Product repeatedly jams at machine transitions.
Containers tip over or fall between conveyors.
Guide rails require frequent adjustment.
Transfer plates become worn or damaged.
Photoeyes are frequently struck or misaligned.
Conveyor chains, belts, or wear strips wear prematurely.
Product scuffing or damage increases.
Jams occur more frequently as line speed increases.
Fingerprints Point Toward the Type of Issue
These fingerprints suggest investigators should examine:
Excessive gaps between conveyors.
Poor elevation alignment between machines.
Inadequate transfer plate design.
Improper guide rail placement.
Conveyor speeds that are not synchronized.
Poor machine spacing.
Product instability during transfer.
Incorrect equipment positioning during installation.
Notice that none of these fingerprints identify the root cause by themselves. They simply narrow the investigation to the machine transition and equipment layout.
Fix-and-Go Issue
Maintenance replaces damaged sensors, adjusts guide rails, repairs conveyors, or clears product jams. Production resumes, but the failures continue because the transfer itself remains unstable. Unless the transition is redesigned or the equipment is properly aligned, the same components will continue to fail.
Correct the Design So It Doesn't Happen Again
Once poor machine transitions have been identified as the root cause, the objective is to create a smooth, controlled transfer of product between machines rather than continually repairing the equipment damaged by recurring jams and impacts. The following engineering improvements address the source of the problem:
Eliminate excessive gaps between adjoining conveyors and equipment.
Align conveyor heights to provide a smooth, uninterrupted product transfer.
Install properly designed transfer plates, dead plates, or powered transfer devices where needed.
Adjust guide rails to maintain consistent product control throughout the transition.
Synchronize conveyor speeds to prevent product collisions, tipping, or gaps in product flow.
Replace worn or damaged transfer components that affect product stability.
Modify conveyor geometry to eliminate abrupt direction changes or unstable product movement.
Increase product support through transition points for unstable or lightweight containers.
Verify that sensors and accumulation controls do not interfere with smooth product flow.
Conduct slow-speed product flow testing after modifications to observe container behavior through each transition.
Monitor transition points during startup, changeovers, and maximum production speeds to verify stable operation.
Standardize transition inspections as part of routine preventive maintenance.
The goal is not simply to eliminate product jams, but to redesign the transition so products move smoothly and consistently from one machine to the next. Stable product flow reduces impacts, minimizes wear on conveyors, guide rails, sensors, and drive components, and significantly improves the reliability of the entire production line.
Prevention and Best Practices
Reliable product flow begins with well-designed machine transitions. Every transfer point should maintain product stability, orientation, and speed while minimizing impact, vibration, and unnecessary handling. Transition design should be treated as a critical reliability requirement, not simply a means of moving product from one machine to the next.
Design transition points to maintain continuous product control from one piece of equipment to the next.
Match conveyor speeds, elevations, and transfer angles to minimize product impact, bouncing, tipping, or sliding.
Minimize transfer gaps by positioning equipment as close together as practical while maintaining adequate maintenance access.
Use properly designed transfer devices such as dead plates, transfer rollers, guide rails, timing screws, star wheels, or powered transfers where appropriate.
Verify that guide rails and product guides maintain consistent product orientation throughout the entire transfer.
Design transitions to accommodate the full range of product sizes, container types, and packaging materials expected on the production line.
Eliminate sharp changes in direction, excessive drop heights, and abrupt speed changes that increase product instability.
Provide adjustment mechanisms that allow transitions to be accurately aligned during product changeovers without excessive trial and error.
Validate product flow during Factory Acceptance Testing (FAT), Site Acceptance Testing (SAT), commissioning, and every major product introduction.
Observe transition performance during startup, changeovers, and maximum production speeds to identify instability before it becomes a chronic problem.
Include transition alignment, guide wear, and transfer device inspections in the preventive maintenance program.
Review recurring jams, damaged product, and equipment wear to determine whether transition design should be improved rather than repeatedly adjusting machine settings.
Every product transfer is an opportunity to either preserve or destroy reliability. When machine transitions are properly designed, products move smoothly through the production line with minimal interruption, reducing jams, product damage, equipment wear, and unnecessary downtime while significantly increasing the Mean Time Between Failures (MTBF) of the entire production system.
Reliability Impact
Poor machine transitions accelerate wear on guide rails, transfer plates, conveyor belts, chains, wear strips, sensors, starwheels, timing screws, and other product-handling components. They also increase product damage, unplanned downtime, maintenance costs, and reduce the MTBF of the entire production line.
3. Poor Drainage and Water Logging
Description and Impact
Electrical equipment generates heat during normal operation. Motors, variable frequency drives (VFDs), PLCs, power supplies, transformers, and electrical panels all rely on adequate ventilation to dissipate that heat. When electrical equipment is installed in confined spaces, positioned too close together, or located near heat-producing equipment without sufficient airflow, operating temperatures rise above their design limits. Elevated temperatures accelerate the deterioration of insulation, electronic components, and electrical connections, reducing equipment life and increasing the likelihood of unexpected failures.
Layout Problem
Electrical equipment is installed without adequate spacing for airflow or is located near ovens, boilers, steam lines, compressors, or other heat-generating equipment. Electrical panels may be positioned against walls, placed in confined spaces, or arranged so closely together that cooling air cannot circulate effectively. These layout decisions trap heat around sensitive electrical components and significantly reduce their service life.

Failure Fingerprints
Motors frequently trip on thermal overload.
VFDs generate overtemperature alarms.
Electrical cabinets feel unusually hot.
Cooling fans run continuously or fail prematurely.
Thermal imaging reveals hot spots inside electrical panels.
Electronic components fail more frequently than expected.
Circuit breakers nuisance trip during periods of high production.
Equipment operates normally when cold but begins faulting as temperatures increase.
Fingerprints Point Toward the Type of Issue
These fingerprints suggest investigators should examine:
Inadequate ventilation around electrical equipment.
Electrical panels installed too close together.
Blocked cabinet ventilation openings.
Dirty or clogged cooling fans and filters.
Heat-producing equipment located adjacent to electrical cabinets.
Inadequate room ventilation or HVAC capacity.
Poor airflow within electrical enclosures.
Excessive ambient operating temperatures.
Fix-and-Go Issue
Maintenance replaces the motor, VFD, cooling fan, power supply, or other failed electrical component. Production resumes, but the replacement operates in the same high-temperature environment and eventually experiences the same failure. Unless the ventilation or equipment layout is corrected, the cycle of overheating and component replacement continues.
Correct the Design So It Doesn't Happen Again
Once poor drainage and water logging have been identified as the root cause, the objective is to eliminate standing water and control its flow rather than continually replacing the equipment it damages. The following engineering improvements address the source of the problem:
Regrade the floor to provide positive drainage toward floor drains.
Install additional floor drains in areas where water routinely accumulates.
Eliminate low spots in the floor that allow water to pool.
Elevate motors, gearboxes, bearings, electrical panels, and other critical equipment above areas exposed to standing water.
Relocate electrical equipment away from washdown zones whenever practical.
Install splash guards, drip shields, or protective covers to prevent water from contacting sensitive equipment.
Route washdown water away from production equipment instead of beneath it.
Repair leaking pipes, hoses, valves, and utility connections that continuously introduce water into the area.
Verify that drain capacity is sufficient to handle washdown volumes without backing up.
Seal floor penetrations and equipment bases where water can infiltrate electrical conduits or structural supports.
Improve housekeeping procedures to remove standing water immediately after washdowns or product spills.
Inspect drains regularly to ensure they remain free of debris and continue to function properly.
The goal is not simply to remove the water after it appears, but to redesign the production line so water has a controlled path away from critical equipment. Effective drainage protects bearings, motors, electrical systems, structural supports, and lubricants from unnecessary deterioration. By eliminating standing water at its source, manufacturers reduce corrosion, prevent moisture-related failures, improve sanitation, and significantly increase the long-term reliability of the production line.
Prevention and Best Practices
Effective drainage should be designed into the production line from the beginning rather than added after water-related failures occur. Proper drainage protects equipment, foundations, utilities, and personnel by preventing standing water from accelerating deterioration and creating unsafe operating conditions.
Design production floors with sufficient slope to direct water toward floor drains and prevent standing water around equipment.
Install floor drains at low points where washdown water, condensate, leaks, or spills are expected to accumulate.
Position equipment, support structures, and utility systems so they do not obstruct water flow to drainage systems.
Elevate motors, electrical panels, control cabinets, junction boxes, and sensitive instrumentation above areas where water may collect.
Route piping, hoses, and utilities to prevent water from dripping directly onto bearings, motors, electrical equipment, or product contact surfaces.
Design machine frames and guarding to eliminate pockets where water can collect and promote corrosion or bacterial growth.
Select corrosion-resistant materials, coatings, and hardware for equipment operating in wet or washdown environments.
Verify that condensate drains, roof drains, and process drainage systems have adequate capacity during peak operating conditions.
Inspect and clean floor drains, trench drains, and drainage channels regularly to prevent blockages and overflow.
Include drainage systems in preventive maintenance inspections to identify erosion, settling, clogged drains, or damaged floor surfaces before they create larger reliability problems.
Verify proper drainage during Factory Acceptance Testing (FAT), Site Acceptance Testing (SAT), commissioning, and after facility modifications.
Reevaluate drainage whenever production equipment is relocated or new processes introduce additional water, cleaning chemicals, or condensate into the operating environment.
Water should never become a chronic operating condition. When drainage is incorporated into the production line design, manufacturers reduce corrosion, prevent premature bearing and electrical failures, improve sanitation, enhance employee safety, and significantly increase the Mean Time Between Failures (MTBF) of the production line.
Reliability Impact
Excessive heat accelerates insulation breakdown, shortens the life of electronic components, increases the frequency of thermal overload trips, and contributes to loose electrical connections through repeated heating and cooling cycles. The result is more unplanned downtime, higher maintenance costs, reduced Mean Time Between Failures (MTBF), and lower overall production reliability.
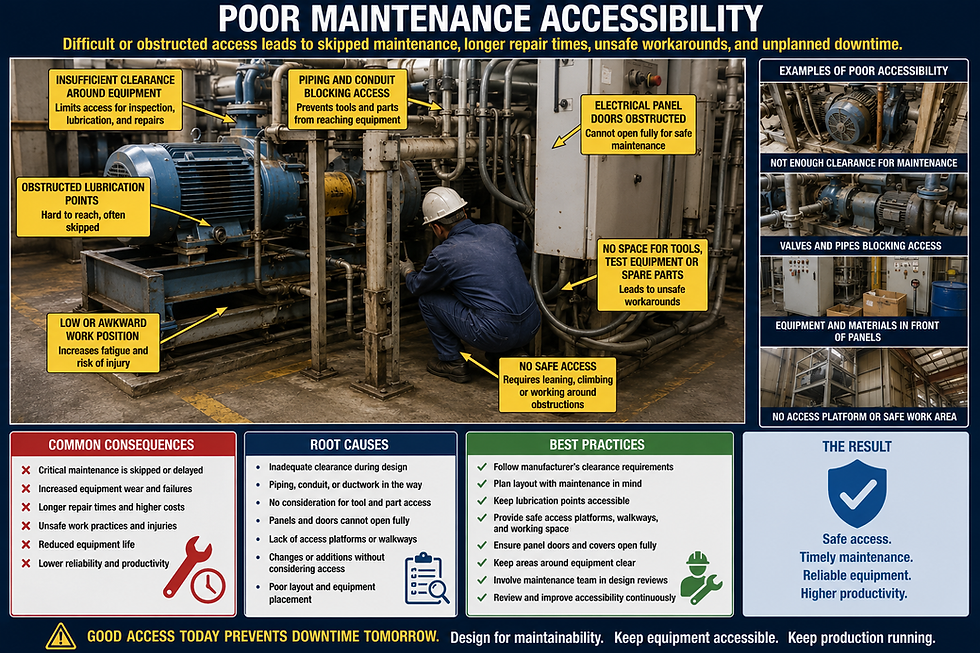
4. Poor Maintenance Accessibility
Description and Impact
Reliability depends on maintenance being performed safely, efficiently, and on schedule. When equipment is installed without adequate access for inspections, lubrication, adjustments, cleaning, or repairs, routine maintenance becomes difficult, time-consuming, or unsafe. As a result, preventive and predictive maintenance tasks are delayed, shortened, or skipped altogether. Over time, normal equipment deterioration accelerates, leading to increased failures across the production line.
Layout Problem
The production line was designed without considering how equipment would be inspected, maintained, or repaired throughout its life cycle. Critical service points are obstructed, cramped, or unsafe to access. Maintenance activities that should take minutes require hours, increasing labor costs and reducing the likelihood that routine preventive maintenance will be completed as scheduled.
Failure Fingerprints
Preventive maintenance tasks are routinely delayed or skipped.
Lubrication points are difficult or unsafe to reach.
Components cannot be inspected without removing guards or adjacent equipment.
Maintenance work takes significantly longer than planned.
Temporary workarounds become common practice.
Equipment is run to failure because repairs are too difficult to perform during scheduled downtime.
Maintenance personnel avoid servicing hard-to-reach components.
The same equipment experiences recurring failures despite repeated repairs.
Fingerprints Point Toward the Type of Issue
These fingerprints suggest investigators should examine:
Inadequate clearance around equipment.
Equipment installed too close to walls or structural columns.
Poor access to lubrication points, motors, gearboxes, or bearings.
Electrical panels or valves blocked by other equipment.
Platforms, walkways, or service areas that are too small or nonexistent.
Maintenance tasks requiring unnecessary disassembly to access routine service points.
Fix-and-Go Issue
Maintenance replaces failed bearings, motors, belts, chains, or sensors as they fail. However, because routine inspections, lubrication, alignments, and adjustments remain difficult to perform, deterioration continues unchecked. The equipment repeatedly fails, not because the replacement parts are defective, but because the layout discourages effective maintenance.
Correct the Design So It Doesn't Happen Again
Once poor maintenance accessibility has been identified as the root cause, the objective is to redesign the work area so routine inspections, lubrication, adjustments, repairs, and component replacements can be performed safely and efficiently. The following engineering improvements address the source of the problem:
Provide adequate clearance around equipment for maintenance personnel and tools.
Reposition equipment to allow safe access to motors, bearings, gearboxes, pumps, valves, and electrical panels.
Relocate lubrication points to accessible locations or install remote lubrication systems.
Ensure guards are designed for quick removal and reinstallation without compromising safety.
Install access platforms, stairs, or walkways where routine maintenance is performed above floor level.
Maintain sufficient clearance for forklifts, cranes, or lifting devices used during component replacement.
Eliminate obstructions that prevent access to electrical disconnects, valves, and emergency shutoffs.
Design piping, conduit, and utility routing so they do not interfere with maintenance activities.
Standardize equipment layouts so similar maintenance tasks are performed consistently across production lines.
Verify that routine preventive and predictive maintenance tasks can be completed without removing adjacent equipment.
Include maintenance personnel during equipment design reviews and factory acceptance testing (FAT) to validate maintainability before installation.
Periodically review maintenance work orders to identify recurring accessibility issues and incorporate improvements into future projects.
The goal is not simply to make repairs easier, but to design equipment so preventive and predictive maintenance can be completed safely, efficiently, and on schedule. When maintenance personnel have safe, unobstructed access to critical components, inspections improve, lubrication is performed consistently, repairs take less time, and equipment deterioration is identified before it becomes an unplanned failure. Designing for maintainability is one of the most effective ways to improve long-term production reliability.
Prevention and Best Practices
Maintainability should be a primary consideration during the design of every production line. Equipment that is difficult to inspect, lubricate, adjust, clean, or repair will inevitably receive less preventive maintenance, leading to accelerated deterioration and reduced reliability.
Involve maintenance, operations, engineering, and safety personnel in production line layout reviews to ensure equipment is designed for long-term maintainability.
Follow the manufacturer's recommended service clearances around motors, pumps, gearboxes, bearings, valves, electrical panels, and other critical components.
Design equipment layouts so routine inspections, lubrication, adjustments, and component replacements can be performed without removing adjacent equipment.
Provide adequate walkways, work platforms, stairs, and safe access points for elevated or confined maintenance activities.
Position lubrication points, inspection ports, gauges, filters, and adjustment mechanisms where they can be safely reached during normal operation.
Ensure guards, access doors, and electrical panel doors can be fully opened without obstruction.
Provide sufficient space for cranes, hoists, forklifts, or lifting devices needed for major component replacements.
Route piping, conduit, cable trays, and utility systems so they do not obstruct maintenance activities or emergency access.
Standardize equipment orientation and maintenance access across similar production lines whenever practical.
Validate maintainability during design reviews, Factory Acceptance Testing (FAT), Site Acceptance Testing (SAT), and commissioning before production begins.
Periodically review preventive maintenance work orders and technician feedback to identify accessibility issues that should be corrected during future upgrades or plant expansions.
Incorporate maintainability reviews into capital projects to ensure new equipment supports safe, efficient, and effective maintenance throughout its service life.
Reliable equipment begins with maintainable equipment. When production lines are designed with maintenance in mind, preventive and predictive maintenance can be performed safely, consistently, and efficiently. The result is better inspections, improved lubrication practices, shorter repair times, reduced unplanned downtime, and significantly higher Mean Time Between Failures (MTBF).
Reliability Impact
Poor maintenance accessibility affects every asset on the production line. Missed inspections, delayed lubrication, skipped adjustments, and deferred repairs accelerate equipment deterioration, increase maintenance costs, reduce Mean Time Between Failures (MTBF), and increase the risk of unexpected breakdowns. A reliable production line is not only designed to operate efficiently—it is designed to be maintained efficiently.
5. Poor Ventilation Around Electrical Equipment
Description and Impact
Electrical equipment generates heat every time it operates. Motors, variable frequency drives (VFDs), PLCs, power supplies, transformers, servo drives, and electrical panels all rely on adequate airflow to dissipate heat and maintain safe operating temperatures. When equipment is installed in confined spaces, placed too close together, or located near ovens, steam lines, or other heat sources without sufficient ventilation, heat becomes trapped around critical electrical components. Elevated operating temperatures accelerate deterioration, shorten component life, and increase the likelihood of unexpected electrical failures.
Layout Problem
The production line was designed without adequate consideration for airflow around electrical equipment. Electrical panels are installed in confined spaces, positioned against walls, clustered together without clearance, or located near heat-generating processes. These layout decisions prevent heat from dissipating effectively, exposing electrical components to temperatures well above their intended operating range.

Failure Fingerprints
Motors repeatedly trip on thermal overload.
VFDs generate overtemperature alarms.
Electrical cabinets feel unusually hot.
Cooling fans run continuously or fail prematurely.
Thermal imaging reveals hot spots inside electrical panels.
Electronic components fail more frequently than expected.
Circuit breakers nuisance trip during periods of high production.
PLCs or control systems experience intermittent faults after prolonged operation.
Equipment operates normally when cold but begins faulting as temperatures increase.
Fingerprints Point Toward the Type of Issue
These fingerprints suggest investigators should examine:
Inadequate ventilation around electrical equipment.
Electrical panels installed too close together.
Blocked cabinet ventilation openings.
Dirty or clogged cooling fans and air filters.
Heat-producing equipment located adjacent to electrical cabinets.
Inadequate room ventilation or HVAC capacity.
Poor airflow within electrical enclosures.
Excessive ambient operating temperatures.
Fix-and-Go Issue
Maintenance replaces motors, VFDs, cooling fans, power supplies, PLC modules, or other failed electrical components. The equipment returns to service, but because the operating environment has not changed, the replacement components are exposed to the same excessive heat and eventually fail again. Unless the ventilation or equipment layout is improved, the cycle of overheating and replacement continues.
Correct the Design So It Doesn't Happen Again
Once poor ventilation has been identified as the root cause, the objective is to reduce operating temperatures by improving airflow rather than continually replacing overheated electrical components. The following engineering improvements address the source of the problem:
Maintain the manufacturer's recommended clearance around electrical panels, motors, VFDs, transformers, and other heat-generating equipment.
Relocate electrical equipment away from ovens, boilers, steam lines, furnaces, and other sources of radiant heat whenever practical.
Improve room ventilation by increasing air circulation or upgrading the HVAC system to handle the electrical heat load.
Install forced ventilation, heat exchangers, or air conditioning units for electrical enclosures operating in high-temperature environments.
Keep cabinet ventilation openings, cooling fans, and filters clean and free from obstructions.
Separate heat-producing equipment from temperature-sensitive electrical and electronic components.
Verify that enclosure ratings are appropriate for the operating environment and do not unnecessarily restrict airflow.
Install temperature monitoring devices in critical electrical panels to identify developing overheating conditions.
Perform routine thermal imaging inspections to identify hot spots before component failure occurs.
Route cables to allow proper airflow within electrical cabinets and avoid overcrowding.
Review equipment loading to ensure motors, drives, and electrical systems are not operating beyond their design capacity.
Verify cooling system performance during peak production periods when electrical loads and ambient temperatures are highest.
The goal is not simply to keep electrical equipment cool, but to create an operating environment where heat is effectively managed throughout the life of the production line. By improving ventilation and controlling operating temperatures, manufacturers extend the life of motors, VFDs, PLCs, electrical connections, and other critical components while reducing thermal overload trips, minimizing unexpected failures, and increasing Mean Time Between Failures (MTBF).
Prevention and Best Practices
The best opportunity to prevent overheating is during the design and layout of the production line. Electrical equipment should be installed in an environment that allows heat to dissipate efficiently while providing safe access for operation and maintenance.
Design electrical rooms and control panels with adequate ventilation to maintain equipment within the manufacturer's recommended operating temperature range.
Maintain the manufacturer's minimum clearance requirements around motors, VFDs, transformers, electrical panels, PLCs, and power supplies.
Locate electrical equipment away from ovens, furnaces, boilers, steam lines, dryers, and other significant heat sources whenever practical.
Size HVAC systems to accommodate the heat generated by electrical equipment during peak production.
Use enclosure cooling systems, heat exchangers, air conditioners, or filtered ventilation where ambient temperatures exceed equipment specifications.
Select electrical enclosures with the appropriate NEMA or IP rating to balance environmental protection with adequate cooling.
Design cable routing to prevent overcrowding inside electrical panels and maintain proper airflow around components.
Install temperature monitoring devices in critical electrical cabinets to detect abnormal operating conditions before failures occur.
Include thermal imaging inspections as part of the preventive and predictive maintenance program to identify developing hot spots.
Regularly inspect and clean ventilation openings, cooling fans, heat exchangers, and air filters to maintain proper airflow.
Verify operating temperatures during Factory Acceptance Testing (FAT), Site Acceptance Testing (SAT), commissioning, and periods of maximum production demand.
Reevaluate cooling capacity whenever new electrical equipment is added or production loads increase to ensure the ventilation system remains adequate.
Proper ventilation is a fundamental requirement for electrical reliability. By controlling operating temperatures through good design and preventive maintenance, manufacturers extend the life of motors, drives, PLCs, electrical connections, and control systems while reducing thermal overload trips, minimizing unexpected failures, and increasing the Mean Time Between Failures (MTBF) of the production line.
Reliability Impact
Excessive heat accelerates insulation breakdown, shortens the life of electronic components, weakens electrical connections through repeated thermal expansion and contraction, and increases the frequency of thermal overload trips. The result is more unplanned downtime, higher maintenance costs, reduced Mean Time Between Failures (MTBF), and lower overall production reliability.
A properly ventilated electrical system is more than an electrical requirement it is a reliability requirement. Managing heat is one of the simplest and most effective ways to extend the life of electrical equipment and improve long-term production performance.
6. Sensors Installed in Harsh Operating Environments
Description and Impact
Sensors are the eyes and ears of a production line. They detect product presence, confirm machine positions, verify process conditions, and provide the feedback required for automated control. When sensors are installed in locations exposed to excessive dust, moisture, vibration, impact, washdown chemicals, or mechanical interference, they become unreliable. Instead of accurately detecting process conditions, they begin producing intermittent or false signals that disrupt production and increase troubleshooting time.
Layout Problem
Sensors are installed where they are exposed to dust, product buildup, moisture, washdown spray, vibration, forklift traffic, or moving equipment. Little consideration was given to protecting the sensor while maintaining a clear detection path. Relocating the sensor, adding protective guarding, or selecting a more suitable mounting location often provides a permanent solution.

Failure Fingerprints
Sensors repeatedly fail before their expected service life.
False product detections occur.
Product passes without being detected.
Intermittent machine stops with no apparent mechanical problem.
Frequent sensor cleaning is required to maintain operation.
Sensor lenses become coated with dust, product residue, or condensation.
Sensor brackets are bent or damaged from repeated contact.
Operators bypass or disable sensors to keep production running.
Fingerprints Point Toward the Type of Issue
These fingerprints suggest investigators should examine:
Poor sensor placement.
Excessive dust or product buildup.
Moisture or washdown exposure.
Mechanical impact from product or equipment.
Excessive vibration.
Improper sensor mounting.
Incorrect sensor technology for the application.
Electrical noise affecting sensor signals.
Fix-and-Go Issue
Replacing the failed sensor often restores production temporarily, but the replacement is exposed to the same harsh conditions and eventually fails for the same reason. Unless the installation location or environmental exposure is corrected, sensor failures will continue to recur.
Correct the Design So It Doesn't Happen Again
Once harsh operating conditions have been identified as the root cause, the objective is to protect sensors from the environment rather than continually replacing damaged or unreliable devices. The following engineering improvements address the source of the problem:
Relocate sensors away from direct exposure to water, steam, chemicals, excessive heat, dust, and product buildup whenever practical.
Select sensors with the appropriate environmental protection rating (IP/NEMA) for the application.
Install protective guards or shields to prevent impact damage from products, pallets, tools, or forklifts.
Mount sensors where they are isolated from excessive vibration and mechanical shock.
Route sensor cables through protective conduit or cable trays to prevent abrasion and accidental damage.
Position sensors where they remain accessible for inspection, cleaning, alignment, and replacement.
Use air purges or protective windows to keep photoelectric sensors free of dust, oil mist, or condensation.
Separate sensor wiring from high-voltage power cables and VFD output cables to minimize electrical interference.
Standardize mounting brackets to simplify alignment and replacement.
Include routine cleaning, alignment verification, and functional testing as part of preventive maintenance.
Verify sensor performance during startup, changeovers, washdowns, and peak production conditions.
Review recurring sensor failures to determine whether the operating environment should be modified instead of repeatedly replacing the sensor.
The goal is not simply to install a more robust sensor, but to create an operating environment where sensors can perform reliably throughout their service life. Proper sensor placement and environmental protection improve signal reliability, reduce nuisance machine stops, minimize false alarms, and increase the overall reliability of the production line. When sensors consistently provide accurate information, operators and automated control systems can make the right decisions at the right time.
Prevention and Best Practices
way to prevent sensor failures is to consider the operating environment during the design and installation of the production line. Sensors should be located where they can reliably perform their intended function while being protected from unnecessary environmental exposure and mechanical damage.
Select sensors with the appropriate IP or NEMA environmental rating for the application.
Position sensors away from direct exposure to washdown water, steam, chemicals, excessive heat, dust, oil mist, and product buildup whenever practical.
Install protective guards or shields to prevent impact from products, pallets, tools, forklifts, and maintenance activities.
Mount sensors on rigid, vibration-resistant brackets to maintain alignment and minimize false readings.
Route sensor cables through conduit or protected cable trays to prevent abrasion, crushing, and accidental damage.
Separate sensor wiring from high-voltage power cables and VFD output cables to reduce electromagnetic interference (EMI).
Use air purges, protective windows, or lens covers for photoelectric sensors operating in dusty or wet environments.
Design sensor locations to allow easy access for inspection, cleaning, alignment, testing, and replacement.
Standardize sensor mounting methods and hardware to simplify maintenance and reduce installation errors.
Verify sensor performance during Factory Acceptance Testing (FAT), Site Acceptance Testing (SAT), commissioning, and production startup.
Include routine sensor cleaning, alignment verification, and functional testing in the preventive maintenance program.
Review recurring sensor failures to determine whether environmental conditions or sensor placement should be improved rather than simply replacing the sensor.
Reliable automation begins with reliable sensing. When sensors are selected for the environment and installed in protected, accessible locations, they provide accurate information, reduce nuisance machine stops, improve process control, and significantly increase the Mean Time Between Failures (MTBF) of the production line.
Reliability Impact
Poor sensor placement leads to repeated false signals, nuisance machine stops, missed product detection, unnecessary maintenance, increased troubleshooting time, and reduced equipment availability. Frequent sensor failures create production interruptions, increase maintenance costs, and lower the overall reliability of the production line.
7. Electromagnetic Interference (EMI) from Poor Equipment Placement
Description and Impact
Modern production lines rely on sensors, PLCs, variable frequency drives (VFDs), servo systems, industrial networks, and electronic instrumentation to operate reliably. When high-voltage power cables, VFD output cables, transformers, or motors are installed too close to low-voltage control wiring or communication networks, they can generate electromagnetic interference (EMI). This electrical noise can induce unwanted voltages into adjacent conductors, causing equipment to behave unpredictably. Because EMI is often intermittent, it can be one of the most difficult reliability problems to diagnose.
Layout Problem
High-voltage power wiring, motor leads, and VFD output cables are installed too close to low-voltage control wiring, instrumentation cables, or communication networks. Electrical panels are overcrowded; cable trays lack proper segregation or shielding and grounding practices are inadequate. These layout decisions allow electromagnetic interference to couple into sensitive control circuits.

Failure Fingerprints
PLC inputs randomly change state.
Photoeyes detect product that isn't there.
Variable Frequency Drives (VFDs) trip without an apparent mechanical problem.
HMI communication is occasionally lost.
Industrial Ethernet or fieldbus networks experience intermittent communication errors.
Analog signals fluctuate unexpectedly.
Servo systems lose position.
Equipment runs normally one shift but experiences unexplained faults on another.
Fingerprints Point Toward the Type of Issue
These fingerprints suggest investigators should examine the electrical installation for:
Electromagnetic interference (EMI).
Power and control cables routed together.
VFD output cables installed alongside instrumentation wiring.
Inadequate cable separation.
Improper grounding or bonding.
Missing or damaged cable shielding.
Poor electrical panel wire segregation.
Excessive electrical noise from nearby equipment.
Notice that none of these fingerprints identify the root cause by themselves. They simply narrow the investigation to the electrical installation and wiring layout.
Fix-and-Go Issue
A common response is to replace sensors, PLC input cards, network switches, VFDs, or communication modules because they appear to be malfunctioning. The symptoms often disappear temporarily, only to return because the underlying problem was never corrected. The real culprit may be the physical routing of the electrical system rather than the component itself.
Correct the Design So It Doesn't Happen Again
Once electromagnetic interference (EMI) has been identified as the root cause, the objective is to eliminate the source of electrical noise rather than continually replacing sensors, PLC modules, or other control components. The following engineering improvements address the source of the problem:
Separate high-voltage power cables from low-voltage control, instrumentation, and communication cables.
Route VFD output cables in dedicated cable trays or conduit away from signal wiring.
Install shielded cables where recommended by the equipment manufacturer and ensure shields are properly grounded.
Improve equipment grounding and bonding to eliminate stray electrical currents.
Relocate sensitive electronic equipment away from transformers, large motors, welders, and other sources of electromagnetic noise.
Install ferrite cores, line reactors, or EMI filters where appropriate to reduce electrical interference.
Avoid running power and signal cables in parallel for long distances. Where crossings are necessary, cross them at approximately 90 degrees.
Verify that cable trays are organized to maintain separation between power, control, and communication circuits.
Inspect cable insulation and connectors for deterioration that may increase susceptibility to electrical noise.
Validate signal integrity during equipment commissioning and after major electrical modifications.
Perform periodic inspections of grounding systems, shielding, and cable routing as part of preventive maintenance.
Follow applicable electrical standards and manufacturer installation guidelines for cable separation and grounding.
The goal is not simply to eliminate nuisance electrical faults, but to design an electrical system that provides clean, reliable signals throughout the production line. Proper equipment placement, cable routing, grounding, and shielding reduce electromagnetic interference, improve communication between control devices, minimize unexpected machine stops, and significantly increase the reliability of automated manufacturing systems.
Prevention and Best Practices
Electromagnetic interference (EMI) is best prevented during the design and installation of the production line. Proper equipment placement, cable routing, grounding, and shielding create a stable electrical environment where automation systems can operate reliably without electrical noise disrupting critical signals.
Develop an electrical layout that physically separates high-voltage power circuits from low-voltage control and communication systems.
Route VFD output cables, motor power cables, and high-current conductors in dedicated conduit or cable trays away from instrumentation wiring.
Cross power and signal cables at approximately 90 degrees whenever they must intersect to minimize induced electrical noise.
Use shielded cables where recommended by the equipment manufacturer and terminate cable shields according to industry standards.
Design a single, effective grounding and bonding system to eliminate stray electrical currents and ground loops.
Install EMI filters, line reactors, surge protection devices, or ferrite cores where electrical noise is anticipated.
Locate sensitive equipment such as PLCs, HMIs, instrumentation, and communication hardware away from large motors, transformers, welders, and other high-energy electrical equipment.
Follow manufacturer recommendations for minimum separation distances between power, control, and communication wiring.
Avoid overcrowding electrical panels and cable trays, allowing adequate space for cable organization and future expansion.
Verify signal integrity during Factory Acceptance Testing (FAT), Site Acceptance Testing (SAT), and equipment commissioning.
Perform periodic inspections of grounding systems, cable shielding, conduit, and electrical connections to ensure they remain in good condition.
Document cable routing, grounding points, and electrical layouts to simplify future troubleshooting and system modifications.
Designing with EMI prevention in mind creates a reliable electrical infrastructure that supports stable communication between sensors, PLCs, drives, and control systems. By minimizing electrical noise before production begins, manufacturers reduce nuisance faults, prevent intermittent control problems, improve automation reliability, and increase the Mean Time Between Failures (MTBF) of the entire production line.
Reliability Impact
Electromagnetic interference creates intermittent faults that are difficult to reproduce and diagnose. It leads to nuisance trips, false sensor signals, communication failures, unexpected machine stops, and unnecessary replacement of perfectly functional components. Frequent production interruptions, repeated equipment restarts, and extended troubleshooting time reduce equipment availability, increase maintenance costs, and ultimately lower overall production reliability.
8. Poor Utility Routing
Description and Impact
Production equipment depends on utilities such as electricity, compressed air, water, steam, hydraulic oil, natural gas, process chemicals, and communication cables. When these utilities are routed without considering equipment operation, maintenance access, environmental conditions, or future expansion, they become a source of recurring equipment failures. Utility lines that cross walkways, obstruct maintenance activities, rub against moving equipment, or expose electrical systems to moisture increase deterioration and reduce equipment reliability.
Layout Problem
The production line was designed without fully considering how utilities would interact with equipment throughout its life cycle. Electrical, pneumatic, hydraulic, steam, and water systems are routed where they are exposed to heat, vibration, moisture, mechanical damage, or routine maintenance activities. Instead of supporting reliable operation, the utilities become another source of equipment deterioration.

Fingerprints
Air leaks develop repeatedly in the same locations.
Hydraulic hoses show signs of abrasion or wear.
Electrical conduits become damaged or bent.
Water drips onto motors, bearings, or electrical panels.
Steam lines overheat nearby electrical equipment.
Communication cables experience intermittent signal loss.
Utility lines interfere with maintenance activities.
Flexible hoses kink, crack, or fail prematurely.
Electrical panels show evidence of moisture intrusion.
Temporary repairs to utility lines become common.
Fingerprints Point Toward the Type of Issue
These fingerprints suggest investigators should examine:
Utility lines routed too close to moving equipment.
Electrical conduits exposed to impact or vibration.
Water, steam, or chemical lines positioned above electrical equipment.
Inadequate support or protection for piping and conduit.
Utility crossings that obstruct maintenance access.
Flexible hoses subjected to repeated bending or rubbing.
Poor separation between power, control, and communication cables.
Utility routing that exposes equipment to leaks or contamination.
Fix-and-Go Issue
Maintenance replaces leaking hoses, damaged cables, failed sensors, motors, electrical components, or pneumatic fittings. Production resumes, but because the utilities remain improperly routed, the same failures continue to occur. Unless the utility routing is redesigned, maintenance simply repeats the same repairs.
Correct the Design So It Doesn't Happen Again
Once poor utility routing has been identified as the root cause, the objective is to redesign the utility systems, so they support reliable equipment operation instead of contributing to equipment deterioration. The following engineering improvements address the source of the problem:
Route electrical, pneumatic, hydraulic, steam, water, gas, and process piping away from moving machine components.
Prevent water, steam, or chemical lines from passing directly over motors, bearings, electrical panels, PLCs, and control cabinets whenever practical.
Support piping, conduit, and cable trays adequately to prevent sagging, vibration, and mechanical stress.
Separate power, control, and communication cables to minimize electrical interference and simplify troubleshooting.
Install drip legs, drip pans, or protective shielding where leaks could damage production equipment.
Protect utilities from forklift traffic, maintenance activities, and accidental impact by using guards, bollards, or elevated routing.
Route flexible hoses to eliminate excessive bending, twisting, rubbing, and pinch points.
Install isolation valves and disconnects where utilities can be safely serviced without shutting down the entire production line.
Clearly identify and label utility lines to improve maintenance efficiency and reduce the risk of servicing errors.
Design utility routing to provide unobstructed access to equipment for inspections, lubrication, repairs, and component replacement.
Inspect utility supports, clamps, hangers, and protective coverings regularly to identify deterioration before failures occur.
Review utility routing whenever equipment is relocated or production lines are expanded to ensure the routing continues to support reliable operation.
The goal is not simply to organize utilities, but to integrate them into the production line so they protect—not compromise—equipment reliability. Well-routed utilities reduce mechanical damage, prevent moisture intrusion, simplify maintenance, improve safety, and ensure that electrical, pneumatic, hydraulic, and process systems support long-term reliable operation instead of becoming recurring sources of failure.
Prevention and Best Practices
The most effective way to prevent utility-related reliability problems is to incorporate utility routing into the production line design process rather than treating it as an afterthought. Well-designed utility systems improve equipment reliability, maintenance efficiency, safety, and future expandability.
Develop a utility routing plan during the initial production line layout that includes electrical, pneumatic, hydraulic, steam, water, gas, chemical, and communication systems.
Route utilities to avoid moving machine components, high-traffic areas, and locations where they are susceptible to impact or abrasion.
Separate electrical power cables from control and communication wiring to reduce electromagnetic interference (EMI).
Avoid routing water, steam, and chemical lines directly above motors, bearings, electrical panels, PLCs, or control cabinets.
Install adequate supports, hangers, clamps, and cable trays to prevent vibration, sagging, and mechanical stress.
Protect utilities with guards, bollards, or overhead routing where forklifts, carts, or maintenance activities could cause damage.
Design utility systems with sufficient clearance to allow safe inspections, preventive maintenance, and equipment replacement.
Install isolation valves, disconnects, and quick-connect fittings to simplify maintenance and minimize production downtime.
Clearly label utility lines, flow direction, and isolation points to improve troubleshooting and reduce maintenance errors.
Design utility routing to accommodate future equipment additions and production line expansions without major rework.
Inspect utility supports, piping, conduit, hoses, and cable trays regularly for signs of wear, corrosion, leaks, vibration, or damage.
Review utility routing whenever production equipment is relocated or modified to ensure the system continues to support reliable operation.
Proper utility routing is an essential part of production line design. When utilities are organized, protected, and accessible, they support reliable equipment operation instead of becoming a recurring source of leaks, electrical failures, maintenance delays, and unnecessary downtime.
Reliability Impact
Poor utility routing accelerates hose failures, electrical faults, communication problems, moisture damage, corrosion, and mechanical wear. It increases maintenance time, creates additional safety hazards, and reduces Mean Time Between Failures (MTBF). Proper utility routing protects critical systems, improves maintainability, and ensures that utilities support reliable production instead of becoming a recurring source of failure.
9. Improper Equipment Spacing
Description and Impact
Adequate spacing between equipment is essential for reliable production. During the design phase, sufficient clearance must be provided for equipment operation, maintenance access, ventilation, product flow, cleaning, inspections, and future repairs. When machines are installed too close together, they compete for space, restrict airflow, increase vibration transmission, limit maintenance access, and create unsafe working conditions. What may appear to save floor space during installation often results in years of reduced reliability and increased maintenance costs.
Layout Problem
The production line was designed to maximize floor space rather than long-term reliability and maintainability. Machines are installed with minimal clearance, leaving insufficient room for airflow, inspections, repairs, cleaning, and safe access. As equipment ages, these space constraints increase maintenance time, reduce preventive maintenance effectiveness, and contribute to recurring failures.

Failure Fingerprints
Maintenance personnel cannot safely access components.
Bearings, motors, and drives operate at elevated temperatures.
Vibration transfers from one machine to another.
Product accumulates or becomes unstable between machines.
Guards cannot be fully opened for inspections or repairs.
Electrical panels are difficult to access.
Frequent damage occurs during maintenance activities due to limited working space.
Components require unnecessary disassembly to reach routine service points.
Equipment modifications become difficult because of limited clearance.
Fingerprints Point Toward the Type of Issue
These fingerprints suggest investigators should examine:
Inadequate clearance between adjacent equipment.
Insufficient working space for maintenance activities.
Restricted airflow around motors, drives, and electrical panels.
Equipment positioned too close to walls, columns, or other structures.
Limited access to lubrication points, valves, and electrical disconnects.
Insufficient space for product accumulation or operator movement.
Poor consideration for future maintenance or equipment replacement.
Fix-and-Go Issue
Maintenance repeatedly replaces overheated motors, damaged sensors, worn bearings, or other failed components while working in cramped conditions. Repairs take longer than necessary, inspections are shortened, and preventive maintenance is often deferred because of poor accessibility. The equipment returns to service, but the underlying layout continues to accelerate deterioration.
Correct the Design So It Doesn't Happen Again
Once improper equipment spacing has been identified as the root cause, the objective is to redesign the production line so each machine has sufficient space to operate, be maintained, and perform reliably throughout its life cycle. The following engineering improvements address the source of the problem:
Reposition equipment to provide adequate clearance for operation, inspections, maintenance, and repairs.
Maintain the manufacturer's recommended service clearances around motors, gearboxes, electrical panels, pumps, and other critical components.
Provide sufficient airflow around motors, drives, electrical cabinets, and other heat-generating equipment.
Ensure guards, access doors, and electrical panel doors can fully open without obstruction.
Allow enough space for lifting devices, forklifts, hoists, or cranes used during component replacement.
Design adequate operator walkways and maintenance access paths to improve safety and efficiency.
Separate equipment sufficiently to reduce the transmission of vibration between adjacent machines.
Provide adequate space for product accumulation, changeovers, and normal operating adjustments.
Leave room for future equipment upgrades, expansion, or technology improvements without requiring a complete production line redesign.
Verify that piping, conduit, cable trays, and utilities do not restrict access or reduce equipment clearances.
Review equipment spacing during design reviews, Factory Acceptance Testing (FAT), and Site Acceptance Testing (SAT) to confirm maintainability before startup.
Conduct periodic reviews after production begins to identify areas where congestion is reducing maintenance efficiency or equipment reliability.
The goal is not simply to create more floor space, but to provide each piece of equipment with the operating and maintenance clearances necessary for long-term reliability. Proper equipment spacing improves airflow, reduces vibration transfer, simplifies maintenance, enhances operator safety, shortens repair times, and significantly increases the Mean Time Between Failures (MTBF) of the entire production line.
Prevention and Best Practices
The best opportunity to prevent equipment spacing issues occurs during the design and layout phase of a production line. Providing adequate space from the beginning improves safety, maintainability, equipment life, and overall production reliability.
Design equipment layouts using the manufacturer's recommended operating and maintenance clearances.
Involve maintenance, operations, engineering, and safety personnel during the layout review to ensure adequate access throughout the equipment life cycle.
Verify that motors, gearboxes, pumps, bearings, valves, and electrical panels can be inspected, serviced, and replaced without moving adjacent equipment.
Provide sufficient airflow around motors, VFDs, electrical cabinets, and other heat-generating equipment to prevent overheating.
Allow adequate space for forklifts, cranes, hoists, or other lifting devices required for major component replacement.
Design operator walkways and maintenance access routes that remain unobstructed during normal production.
Ensure guards, electrical panel doors, and access covers can be fully opened without interference.
Leave adequate clearance for piping, conduit, cable trays, and utility systems without restricting maintenance access.
Design sufficient product accumulation and transition space to maintain stable product flow between machines.
Isolate equipment that generates significant vibration to minimize vibration transmission to adjacent assets.
Reserve space for future equipment upgrades, process modifications, and production expansion.
Validate equipment spacing during design reviews, Factory Acceptance Testing (FAT), and Site Acceptance Testing (SAT) before production begins.
Periodically evaluate equipment spacing after process changes to ensure modifications have not compromised accessibility, airflow, or maintainability.
Proper equipment spacing is an investment in long-term reliability. Production lines should be designed not only to fit within the available floor space, but also to allow equipment to be operated, inspected, maintained, and upgraded safely and efficiently throughout its entire service life.
Reliability Impact
Improper equipment spacing increases maintenance labor, restricts ventilation, transfers vibration between machines, reduces inspection quality, and accelerates equipment deterioration. It results in more unplanned downtime, higher maintenance costs, and reduced Mean Time Between Failures (MTBF). Reliable production lines are designed with enough space not only to operate efficiently but also to be safely maintained throughout their service life.
Proper equipment spacing is an investment in reliability. The space designed into a production line today becomes the maintenance efficiency and equipment reliability achieved for years to come.
10. Poor Piping Design Causing Backpressure
Description and Impact
Process piping is designed to transport liquids, gases, steam, and compressed air at the required pressure and flow rate. When piping systems are undersized, contain excessive bends, unnecessary restrictions, improper elevations, or poorly located valves, resistance to flow increases. This creates backpressure, forcing pumps, compressors, and process equipment to work harder than intended. The additional load accelerates equipment deterioration, reduces efficiency, and shortens equipment life.
Layout Problem
The production line was designed with piping that cannot efficiently deliver the required flow. Poor routing, undersized pipe, excessive restrictions, unnecessary fittings, or improper system design create backpressure throughout the process. Instead of supporting efficient production, the piping system forces equipment to operate under unnecessary stress every day.

Failure Fingerprints
Pumps experience repeated seal failures.
Motors draw higher-than-normal amperage.
Flow rates are inconsistent or below design capacity.
Pressure gauges show unusually high upstream pressure.
Relief valves open frequently.
Pumps cavitate or produce excessive noise.
Pipe vibration increases during operation.
Filters require replacement more often than expected.
Energy consumption gradually increases.
Process performance varies between production runs.
Fingerprints Point Toward the Type of Issue
These fingerprints suggest investigators should examine:
Undersized piping.
Excessive elbows, tees, or unnecessary fittings.
Long pipe runs creating excessive friction losses.
Improper valve selection or partially restricted valves.
Poor piping elevations or routing.
Blocked strainers or filters.
Inadequate system capacity.
Improperly designed process flow paths.
Fix-and-Go Issue
Maintenance replaces pump seals, bearings, motors, valves, or compressors that repeatedly fail under excessive operating loads. The equipment returns to service, but because the piping system continues to restrict flow, the replacement components are subjected to the same conditions and fail again. Unless the piping design is corrected, recurring failures are inevitable.
Correct the Design So It Doesn't Happen Again
Once poor piping design has been identified as the root cause, the objective is to eliminate unnecessary flow restrictions rather than continually replacing pumps, seals, valves, or motors damaged by excessive backpressure. The following engineering improvements address the source of the problem:
Verify that piping is properly sized to deliver the required flow rate with acceptable pressure losses.
Eliminate unnecessary elbows, tees, reducers, and fittings that increase friction losses.
Shorten excessive pipe runs whenever practical to reduce flow resistance.
Replace undersized piping that restricts system capacity.
Select valves with the appropriate flow characteristics and ensure they are correctly sized for the application.
Minimize abrupt changes in pipe diameter by using gradual reducers and expanders where appropriate.
Improve piping layouts to create smoother, more direct flow paths.
Properly support piping to prevent sagging, vibration, and excessive mechanical stress on pumps and equipment connections.
Install pressure gauges and flow meters at critical locations to monitor system performance and detect developing restrictions.
Routinely inspect and clean strainers, filters, and heat exchangers that contribute to pressure losses.
Verify pump selection and operating curves to ensure equipment is operating within its Best Efficiency Point (BEP).
Review piping modifications whenever production capacity is increased to ensure the system can accommodate the additional demand.
The goal is not simply to reduce system pressure, but to design a piping system that allows fluids to move efficiently with minimal resistance. Proper piping design reduces pump loading, minimizes cavitation, lowers energy consumption, extends the life of seals, bearings, valves, and motors, and significantly improves the long-term reliability of the entire production process.
Prevention and Best Practices
The most effective way to eliminate backpressure is to design the piping system correctly before production begins. The following best practices help ensure efficient flow, protect equipment, and improve long-term reliability:
Perform hydraulic calculations during the design phase to verify required flow rates, pressures, and pipe sizing.
Size piping based on process demand, future capacity, and acceptable pressure losses rather than minimum installation cost.
Design piping runs to be as short and direct as practical.
Minimize unnecessary elbows, tees, valves, and fittings that increase friction losses.
Select pumps that operate near their Best Efficiency Point (BEP) for the expected operating conditions.
Specify valves with the proper flow characteristics and pressure ratings for the application.
Provide adequate pipe supports to prevent vibration, sagging, and mechanical stress.
Design systems with sufficient access for cleaning, inspection, and maintenance of valves, strainers, filters, and instrumentation.
Install pressure gauges, flow meters, and differential pressure indicators at strategic locations to monitor system performance.
Include isolation valves and bypass arrangements where maintenance can be performed without shutting down the entire production line.
Review piping layouts during design reviews, Factory Acceptance Testing (FAT), and Site Acceptance Testing (SAT) to verify efficient flow paths.
Evaluate piping modifications whenever production rates or process requirements change to ensure the system remains properly sized.
Incorporate predictive maintenance practices by monitoring pressure, flow, pump amperage, vibration, and energy consumption to detect developing restrictions before equipment failure occurs.
Periodically inspect the system for fouling, scaling, product buildup, corrosion, and partially closed valves that increase flow resistance.
Proper piping design is more than moving fluids from one point to another it is about delivering the required flow with the least possible resistance. A well-designed piping system reduces energy consumption, minimizes equipment loading, extends the life of pumps and valves, and provides the stable operating conditions necessary for long-term production reliability.
Reliability Impact
Backpressure increases pump loading, motor temperatures, seal wear, bearing failures, valve deterioration, and energy consumption. It reduces process efficiency, increases maintenance costs, and shortens Mean Time Between Failures (MTBF). A properly designed piping system minimizes flow resistance, protects equipment, and allows the entire production line to operate as intended.
Reliable production depends on more than the equipment itself. When the piping system is designed correctly, pumps, compressors, and process equipment operate within their intended limits, improving both performance and long-term reliability.
Final Thoughts
Your production line layout directly affects equipment reliability and MTBF. These failure fingerprints reveal hidden design flaws that cause repeated breakdowns and inefficiencies. By identifying and addressing these issues, such as improving alignment, access, ventilation, and flow you can extend equipment life, reduce downtime, and boost overall productivity.
Start by observing your line for these fingerprints. Engage your maintenance and operations teams to gather insights. Then prioritize layout changes that target the root causes. Small adjustments can lead to big improvements in reliability and cost savings.
Taking a proactive approach to production line design will help your facility run smoother and keep your equipment running longer.


Comments